
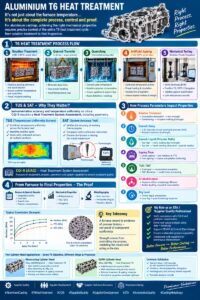
It’s not just about the furnace temperature. It’s about the complete process, control, validation, and proof.
In aluminium casting, achieving the required mechanical properties depends on controlling the entire T6 heat-treatment cycle.
JUFENG Precision — As an Aluminium Casting and Supplier Quality professional, we focus on these critical checkpoints:
🔹 Solution Treatment — Temperature uniformity, soak time, and alloy-specific process limits.
🔹 Quench Transfer & Quenching — Transfer delay, cooling conditions, distortion, and cracking risks.
🔹 Artificial Ageing — Validated time-temperature parameters to achieve the required properties.
🔹 Pyrometry: TUS & SAT — Furnace temperature uniformity and measurement-system accuracy, where applicable.
🔹 Product Validation — Hardness, tensile properties, metallography, and traceable process records.
Application-specific experience:
▪️ Rheocasting cylinder head — AlSi10MgCu0.5, T6
▪️ GSPM cylinder head — AlSi7Mg, T6
Although both applications use T6 heat treatment, their alloy chemistry and casting processes require appropriate process validation.
Our STA takeaway:
A furnace record is evidence of process history—not, by itself, proof of component conformity.
Sustainable supplier quality comes from connecting process parameters with metallurgical evidence, mechanical-test results, root-cause analysis, and continuous improvement.
Better Process → Better Casting → Better Performance.
This technical sharing is brought to you by JUFENG Precision.
How do you correlate heat-treatment parameters with mechanical properties in your aluminium casting process?
 English
 Chinese
 German
 Spanish
 French
 Polish
 Portuguese
 Japanese
 Vietnamese
 Thai
 Russian
 Arabic
 Korean